
NEO MAKİNA ve MÜHENDİSLİK A.Ş. designs and manufactures industrial deaerator systems that remove dissolved oxygen and carbon dioxide from boiler feed water, and condensate tanks and pump sets that collect and recover condensate. Systems comprising thermal deaerator, feed-water tank, condensate tank, flash vessel and pump stations protect boiler and piping from oxygen corrosion while recovering condensate heat to cut fuel and water consumption.
Thermal Deaerator Systems
Operating Principle
By Henry's Law, gas solubility in water falls as temperature rises. In the deaerator, feed water is heated to saturation (104–105 °C at 0.2–0.3 bar) by counter-current steam through spray nozzles and a packed/tray column; released O₂ and CO₂ are vented to atmosphere with the vent steam. Outlet oxygen is reduced below 7 µg/L (0.007 ppm); chemical oxygen-scavenger consumption is minimised.
Technical Features
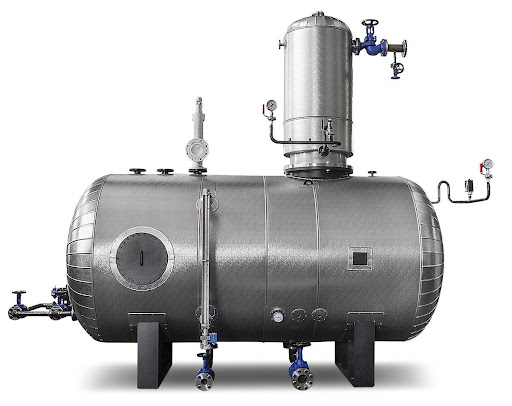
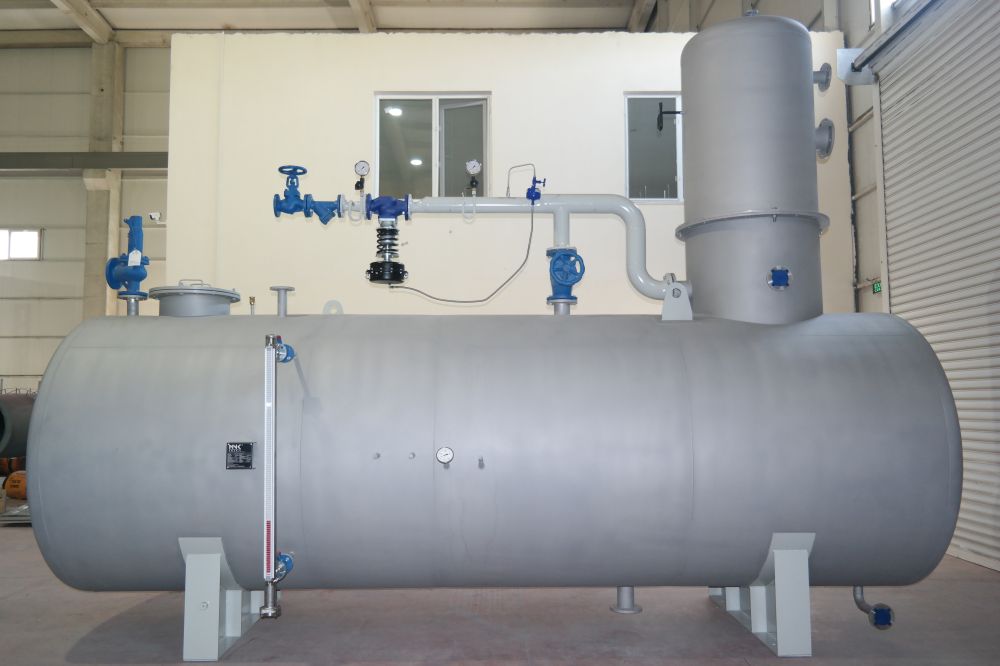
- Types: Spray, tray and packed-column deaerators; vertical column mounted on a horizontal storage tank.
- Capacity: 500 – 50,000 kg/h feed water; modular design for peak loads.
- Operating pressure: 0.2 – 0.5 bar (g); 0.1–1.0 bar on a project basis.
- Materials: Column and spray section AISI 304L/316L stainless; storage tank P265GH carbon steel or stainless; insulation and cladding.
- Equipment: Steam pressure-regulating valve, level control valve, safety valve, vacuum breaker, overflow and blowdown connections, sampling.
- Automation: PLC control of level, temperature and pressure; integration with boiler automation; remote monitoring.
- Standards: PED 2014/68/EU, EN 13445 / AD 2000, CE
Condensate Systems: Energy Recovery
Condensate is the most valuable feed water returned to the boiler: treated, chemically conditioned and 80–100 °C hot. Every 10% of condensate return saves roughly 1–1.5% boiler fuel and the same proportion of water and chemicals.
Condensate Tanks
- Atmospheric tanks: For unpressurised return lines; economical solution with vent, level gauge and overflow.
- Pressurised condensate tanks: Hold hot condensate under pressure to prevent flash-steam loss; closed-loop return.
- Flash vessels: Generate low-pressure steam from high-pressure condensate for reuse in the process.
- Materials: AISI 304/316 stainless or carbon steel; insulated; 0.5 – 50 m³ volume.
Condensate Pump Sets
- Centrifugal pumps: High flow, low head; low-NPSH design for hot condensate, 1+1 standby.
- Positive-displacement pumps: Low flow, high head; high volumetric efficiency.
- Mechanical condensate pumps: Steam- or air-driven, no electricity; no cavitation risk, return from remote points.
- Construction: Cast iron or stainless casing; hot-water mechanical seal; variable-speed level control.
Typical Application Range
- Deaerator capacity: 500 – 50,000 kg/h; condensate tank 0.5 – 50 m³; pump flow 1 – 100 m³/h
- Applications: steam boiler houses, textile, food, chemical, paper, power plants, petrochemical, hospital and hotel steam systems
- Scope: deaerator + feed-water tank + condensate tank + pumps + valves and instrumentation on a single skid
Why NEO MAKİNA?
As a boiler manufacturer we size the deaerator, condensate and feed-water system together with the boiler heat balance: steam consumption, condensate return ratio, flash-steam utilisation and feed-water temperature are calculated to select the optimum configuration. Deaerator additions, condensate-recovery lines and pump replacement are carried out as retrofits in existing boiler houses. For boiler solutions see Water-Tube Hybrid Steam Boilers.
Frequently Asked Questions
When is a deaerator required?
It is standard for corrosion protection on boilers above 10 bar and plants with low condensate return (high make-up); for small boilers a 90 °C feed tank plus chemical oxygen scavenger may suffice.
How much vent steam does a deaerator lose?
About 0.5–1% of feed water is vented as steam; a vent condenser recovers this heat for make-up water preheating.
How can condensate return be increased?
Steam-trap selection and maintenance, closed pressurised condensate lines, mechanical condensate pumps and flash-steam recovery can raise return to 80–90%; a site survey is carried out at proposal stage.
For deaerator and condensate system design and a quotation for your steam system, contact us.